Miniature electromagnetic assemblies in consumer electronics, industrial sensors, automotive electronics and robotics demand compact, complex‑geometry soft‑magnetic parts. Traditional stamping and lamination are limited to simple 2‑D flat shapes, while conventional press‑and‑sinter powder metallurgy struggles to deliver intricate multi‑feature 3‑D structures. Metal Injection Molding (MIM) opens new possibilities to manufacture near‑net‑shape soft‑magnetic components with integrated mounting bosses, holes, flux‑guide contours and assembly interfaces.
Nevertheless, soft‑magnetic MIM parts are not “regular metal parts with magnetic properties”. Final magnetic performance heavily depends on powder quality, sintered density, residual carbon / oxygen content, stress‑relief annealing, part geometry and air‑gap control. Copying soft‑magnetic datasheets of wrought alloys directly onto MIM drawings frequently results in unstable permeability, high coercivity and inconsistent electromagnetic response in mass‑production.
This article explains mainstream soft‑magnetic MIM alloy grades, key property comparison, design & tolerance control tips, suitable surface treatments, a real‑world manufacturing case, and practical sourcing guidance for electronic‑industry soft‑magnetic MIM projects.
What Are Soft‑Magnetic MIM Materials? Key Pros and Typical Electronic Uses
Soft‑magnetic MIM materials are iron‑based sintered alloys that can be easily magnetized and demagnetized under external magnetic fields, with low coercivity and minimal residual magnetism. They are widely used for solenoid cores, armatures, sensor yokes, relay pole pieces, flux guides and miniature electromagnetic actuators for electronics and mechatronic devices.
Major commercial soft‑magnetic MIM grades include Fe‑3%Si silicon‑iron, Fe‑50Ni permalloy, Fe‑49Co‑2V (Fe‑Co) alloy. Each grade differs in saturation flux density, permeability, coercivity, electrical resistivity, machinability and material cost.
Fe‑3%Si (Silicon‑Iron MIM)The most cost‑effective soft‑magnetic MIM option. Delivers high saturation magnetization and excellent electrical resistivity to suppress eddy‑current losses. Best‑suited for medium‑frequency solenoids, miniature motor cores and general‑purpose electromagnetic actuators in consumer electronics.
Fe‑50Ni (Permalloy MIM)Features extremely high magnetic permeability and ultra‑low coercivity. Ideal for high‑sensitivity magnetic‑sensor components, magnetic shielding parts and precision relay assemblies where weak‑field response is critical.
Fe‑49Co‑2V (Fe‑Co MIM)Offers the highest saturation magnetic flux density among commercial soft‑magnetic MIM alloys. Applied in compact high‑flux electromagnetic components where limited space requires maximum magnetic output. Higher raw‑material cost restricts it to high‑performance niche projects.
Ferritic Stainless 430L MIMProvides moderate soft‑magnetic performance combined with improved corrosion resistance. Selected when magnetic function and environmental corrosion exposure co‑exist.
Key Properties Comparison for Soft‑Magnetic MIM Alloys
Note: All values reference high‑density (≥96 %) sintered and fully annealed MIM specimens. Actual performance will degrade with rising porosity, residual stress, carbon / oxygen contamination.
| Property | Fe‑3%Si | Fe‑50Ni (Permalloy) | Fe‑49Co‑2V | 430L Ferritic Stainless |
|---|
| Saturation Flux Density (T) | ~2.0 | ~1.5 | ~2.4 | ~1.4 |
| Maximum Relative Permeability | Medium | Very High | High | Low‑Medium |
| Coercivity Hc (A/m) | 80‑120 | 2‑5 | 15‑30 | 120‑200 |
| Electrical Resistivity | High | Medium | Low | Medium |
| Anti‑Eddy‑Current Performance | Excellent | Good | Fair | Good |
| Corrosion Resistance | Poor | Poor | Poor | Good |
| Material Cost | Low | High | Very High | Medium |
| Typical Application | Solenoid cores, actuator armatures | Precision sensors, magnetic shielding | High‑flux compact electromagnetic parts | Magnetic parts under humid environment |
| Main Process Requirement | Controlled sintering + hydrogen annealing | Strict impurity control + stress‑relief annealing | Low‑impurity feedstock, precise thermal cycle | Vacuum sintering |
How to Control Distortion, Tolerance and Magnetic‑Performance Consistency
Soft‑magnetic MIM components are highly sensitive to residual stress. Sinter‑induced distortion, clamping stress during CNC secondary sizing and improper heat‑treatment will degrade permeability and raise coercivity, ruining electromagnetic performance even if all dimensional measurements look correct.
Tolerance allocation guidelines for electronic soft‑magnetic MIM parts
Magnetic‑pole / air‑gap mating surfaces: Tight tolerance ±0.02‑0.03 mm. These surfaces directly determine electromagnetic air‑gap size; define flatness and parallelism requirements explicitly on drawings.
Mounting holes & positioning features: ±0.05‑0.10 mm, moderate tolerance to balance cost and assembly accuracy.
Non‑critical outer contours & internal pockets: ±0.10‑0.20 mm, adopt looser tolerance to cut manufacturing cost.
Critical design tips to avoid distortion & magnetic‑performance drift
Avoid extreme thin unsupported walls: Maintain minimum wall thickness ≥1.0 mm; limit unsupported wall height‑to‑thickness ratio ≤8:1 to reduce sinter sagging and warpage.
Prefer balanced, symmetric geometry: Asymmetric parts produce uneven sinter shrinkage, resulting in pole‑face tilt and unstable air gaps. Add transition fillets (R ≥1.5 mm) for abrupt wall‑thickness changes.
Reserve post‑machining stress‑relief annealing: Any CNC sizing operation introduces residual stress. Stress‑relief annealing must be performed after secondary machining to restore soft‑magnetic properties.
Clearly define magnetic acceptance criteria on drawings: Specify test frequency, coercivity, permeability, saturation flux and test sample position. Do not only specify alloy grade as acceptance standard.
Choose Suitable Surface Treatments for Soft‑Magnetic MIM Electronic Components
Surface treatment selection must balance corrosion protection and electrical‑magnetic function. Some coatings will insulate mating pole surfaces or introduce residual stress, worsening electromagnetic performance.
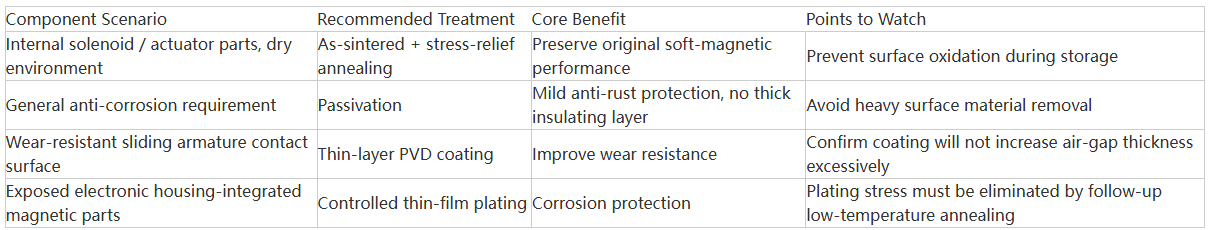
Important warning: Hard anodizing is generally NOT recommended for functional magnetic pole surfaces, because thick insulating oxide layers will enlarge the working air gap and reduce electromagnetic output.
Factory Case Study: MIM Fe‑3%Si Solenoid Armature for Industrial Electronic Valves
An industrial electronics customer encountered unstable actuation response with Fe‑3%Si MIM solenoid armatures from their previous supplier. Although dimensional inspection passed, batch‑to‑batch variation of coercivity caused inconsistent valve opening‑and‑closing timing in mass production.
Root‑cause analysis identified two key issues:
Incomplete debinding left residual carbon inside parts, worsening soft‑magnetic performance.
Secondary CNC sizing introduced heavy residual stress, without follow‑up stress‑relief annealing.
Optimized manufacturing workflow implemented:
Optimized multi‑stage solvent‑plus‑thermal debinding profile to strictly control residual carbon content.
Reserved small machining allowance for critical pole surfaces. After CNC sizing, dedicated hydrogen‑atmosphere stress‑relief annealing was executed to eliminate machining‑induced stress and restore magnetic properties.
Added batch sampling magnetic‑performance inspection after final annealing as a formal quality‑control gate before shipment.
Final result: Mass‑produced armatures achieved stable coercivity within target window. All valve actuation timing requirements were satisfied, batch‑to‑batch electromagnetic fluctuation was eliminated for annual volume of 115 000 pieces.
Harbermetal: Your Trusted Magnetic MIM Parts Partner In China
Many engineers select soft‑magnetic MIM alloy grades only from material datasheets, ignoring that sintering impurities, machining residual stress and missing annealing steps can completely ruin magnetic performance of finished components. You do not need to spend multiple sampling cycles debugging magnetic‑property instability. Send your 2D/3D drawings together with electromagnetic functional requirements to Harbermetal. Our engineering team completes DFM review for soft‑magnetic MIM projects, defines annealing, inspection and acceptance criteria before mold investment, helping you avoid costly mass‑production magnetic‑performance failures.
Harber Industrial Limited (Harbermetal) is an ISO‑certified full‑chain Chinese MIM manufacturer with rich hands‑on experience in soft‑magnetic MIM component manufacturing for electronics, sensor and automotive electronic applications. We own complete in‑house workflow: feedstock validation, mold design & fabrication, metal injection molding, multi‑step debinding, precision controlled‑atmosphere sintering, dedicated stress‑relief / hydrogen annealing, secondary CNC sizing and functional surface finishing.
Our engineering team treats soft‑magnetic MIM as a system project instead of only a material‑grade selection: we evaluate geometry symmetry, wall‑thickness distribution, air‑gap‑related critical features, define mandatory post‑machining annealing workflow, and establish batch magnetic‑property inspection gates. We process Fe‑3%Si silicon‑iron, Fe‑50Ni permalloy, 430L ferritic stainless soft‑magnetic MIM parts, and conduct feasibility assessment for Fe‑Co high‑saturation alloys for niche high‑performance projects.
We deliver custom soft‑magnetic MIM solenoid cores, armatures, sensor yokes and relay pole‑piece components for global OEM customers. Magnetic‑test records, dimension inspection reports and batch traceability documents can be provided upon request. Whether you require prototype validation or medium‑to‑high‑volume serial production, Harbermetal balances electromagnetic performance, dimensional stability and total‑project cost.
Contact informationEmail: sales@harber‑mim.comTel: +86 0769‑82389116
Final Thoughts
Soft‑magnetic MIM technology unlocks great design freedom for miniature complex 3‑D electromagnetic components for electronic devices. But alloy name alone cannot guarantee functional performance. Sintered density, impurity control, stress‑relief annealing, geometry symmetry and properly‑defined magnetic acceptance criteria are equally critical.
When developing soft‑magnetic MIM parts, avoid simply migrating wrought‑alloy datasheet parameters. Carry out full‑phase DFM review before tooling investment, mark magnetic‑function‑related critical features and test specifications on drawings. Partnering with an experienced full‑chain MIM manufacturer like Harbermetal can effectively prevent magnetic‑property drift and yield‑loss risks in mass‑production.
Frequently Asked Questions About Magnetic MIM Materials
Q: Is MIM soft‑magnetic performance equal to wrought soft‑magnetic alloy?A: Not completely. Residual porosity, carbon‑oxygen impurities and residual stress in sintered MIM parts will affect permeability and coercivity. Performance reference data must adopt MIM‑specific test standards instead of wrought‑material datasheets. Stress‑relief annealing is essential after any CNC secondary machining.
Q: Can hard‑anodizing be applied to soft‑magnetic MIM pole surfaces?A: Not recommended. Thick anodic oxide layers increase magnetic air gap and weaken electromagnetic output. Passivation or thin‑film PVD coating is preferred for magnetic‑pole functional surfaces.
Q: Why are my MIM soft‑magnetic parts dimensionally OK but magnetically unstable?A: The most frequent causes are residual carbon / oxygen contamination after sintering, or residual stress introduced during CNC secondary machining without subsequent stress‑relief annealing. Magnetic‑property inspection must be arranged after full heat‑treatment.
Q: What is the economical production‑volume range for soft‑magnetic MIM electronic components?A: MIM shows obvious comprehensive‑cost advantages generally starting from 10 000‑20 000 pieces annually. For very‑low‑volume simple‑shape samples, stamping or CNC‑machining of wrought soft‑magnetic alloy may be more cost‑effective.
Ready to start your soft‑magnetic MIM component project? Submit your drawings and functional specifications for a free manufacturability assessment and quotation.
 en
 de
 jp
 kor
 fra
 spa
 ru
 pt
 it







